
How smart, connected lighting boosts efficiency, safety, and sustainability in industrial facilities
It’s no secret that the manufacturing industry has a heavy responsibility for emissions of greenhouse gases. In the US, manufacturing accounts for almost a quarter (23%) of direct carbon emissions, according to the Environmental Protection Agency. In Europe the situation is equally dire: the industry emits an annual total of 880 million tonnes of carbon dioxide equivalents, making it one of the largest emitters of greenhouse gases on the continent. Big changes need to be made across every aspect of manufacturing facilities to make the industry sustainable and future-proof growth.
But its not that simple. The industrial sector faces several challenges: the increasing pressures from ecommerce to produce at speed, the need to stock strategically, the importance of picking accuracy at warehouses, and so on. Broader issues like energy conservation and sustainable operations are also adding pressure on the sector. Gladly, there are (quick) solutions, like connected lighting, that support the digital transformation of any facility.
Challenges faced by industries
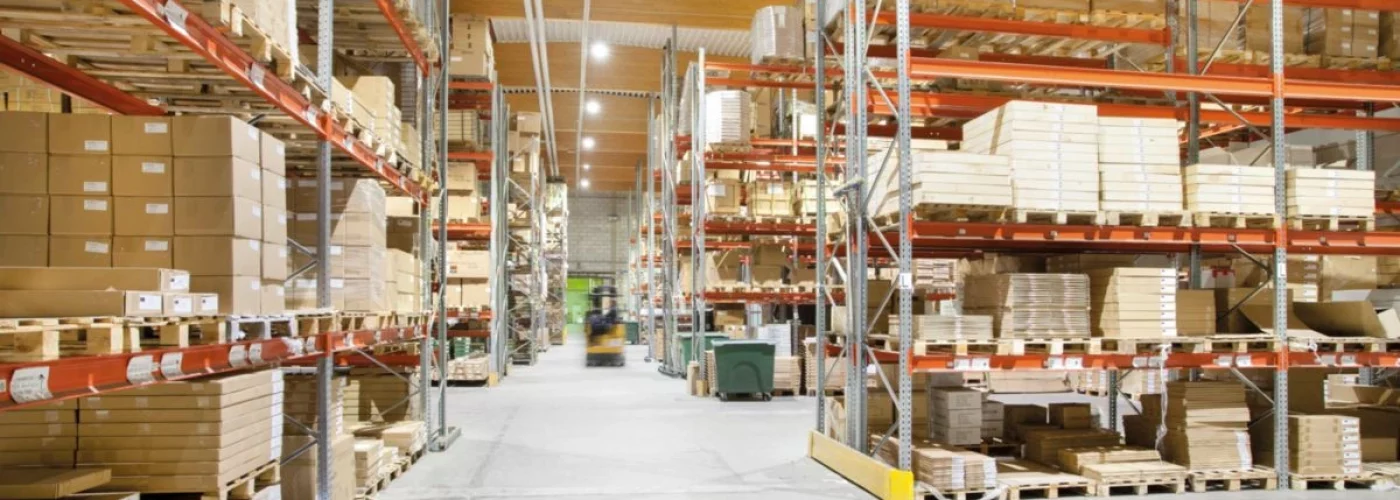
Warehouses, distribution centers, and manufacturing facilities are all tough environments with specific design needs. These include:
- Consistent illumination to ensure smooth operations
Industrial environments present unique lighting challenges, from maintaining consistent illumination across varying mounting heights to providing reliable light levels during long operating hours or to support specific tasks. Research shows that poor lighting can reduce task speed and output quality, while also contributing to unplanned maintenance and costly downtime.
- Enhancing productivity
In an environment where physical work and attention to detail are important, staff fatigue can negatively affect worker accuracy and ultimately reduce productivity. Any space needs to be designed to ensure a safe and productive working environment. Time lost to workplace accidents directly affects productivity and morale across the whole team.
- Delivering the light needed in vital spaces
Manufacturing across the board is becoming increasingly automated. While the range of machinery increases and the technology grows in sophistication, tasks remain the same: people are still required to check, monitor, adjust, maintain, repair, and programme equipment and controls on an ongoing basis.
- Energy efficiency
Industries and factories are known for their substantial energy consumption. 24% of global energy consumption comes from the industrial sector and 5%-20% of annual productivity is lost in the average manufacturing plant due to unplanned downtimes. Also, traditional lighting systems are often inefficient and costly to operate. These should be reviewed, and goals set to reduce waste and improve efficiency.
While the challenges and pressures are many, the good news is that connected lighting can create a safer, more productive working environment for workers in industrial environments.
The role of connected lighting
In the ever-evolving landscape of industrial and factory environments, the role of lighting extends far beyond illumination. Connected lighting solutions like Signify Interact have emerged as a transformative force, offering unprecedented control, efficiency, and sustainability advantages for industries. As industries worldwide strive to optimise operations, reduce energy consumption, enhance workplace safety, and deliver on their digitalisation and decarbonisation strategies, integrating connected lighting has become a strategic imperative.
The right kind of lighting has shown to have a positive impact on production efficiency and quality, employee safety and wellbeing, and a facility’s sustainability and cost efficiency.
Significant energy, carbon, cost, and light quality improvements can be made by simply swapping out inefficient legacy lighting for new efficient LED lighting. LED lighting can be up to 80% more efficient and can last longer than conventional lighting, resulting not only in significant energy and cost savings, but also in reduced maintenance costs, which can be very expensive in industrial facilities with high ceilings.
Taking it a step further, connected LED lighting can play a significant role in enabling a manufacturing facility or a warehouse to become even more digital and sustainable whilst providing a safer, healthier, and more productive place to work. Connected systems, energy-efficient LED luminaires, sensors, and comprehensive wireless system monitoring and management software create an intelligent network. These connected systems enable businesses and building owners to gather valuable data and insights from the facility. This data can then be used to unlock additional value adds, features and benefits
- Lighting asset management
A connected lighting system enables a more proactive approach to maintenance by providing a remote diagnostics dashboard that allows faults to be identified and addressed immediately. It also supports preventive maintenance by using luminaire lifetime data to help schedule servicing before failures occur, while automatic firmware and software updates ensure the system remains secure, up to date, and operating at peak performance.
- Scene management
Intelligent lighting controls deliver the right light at the right time, helping to enhance worker safety and support productivity throughout the facility. Precise lighting schedules can be tailored to different tasks and operational requirements, ensuring optimal illumination where and when it is needed. By automatically dimming lighting in unoccupied or low-use areas, the system also reduces energy consumption, helping businesses progress toward sustainability goals without compromising performance.
- Sustainable operations
Connected lighting has evolved from an energy-saving technology into a strategic sustainability platform. It not only cuts electricity consumption but also provides the data and intelligence needed to optimise building performance, support ESG reporting, improve worker safety and wellbeing, and extend asset life. As manufacturers and logistics operators face increasing pressure to decarbonise while maintaining productivity, connected lighting offers a practical solution that delivers environmental, operational and financial benefits simultaneously.
- Energy optimisation
Gain greater visibility into energy performance across all facilities with comprehensive usage monitoring and reporting. Managed LED lighting solutions can help deliver energy savings of up to 80% by optimising lighting efficiency and reducing unnecessary consumption. By comparing performance across multiple sites, businesses can benchmark usage, identify improvement opportunities, and make data-driven decisions to maximise energy savings and support sustainability goals.
- Remote testing with emergency lighting
Connected lighting can significantly improve the management of emergency lighting by enabling remote testing, monitoring and reporting, helping organisations maintain compliance while reducing maintenance costs and operational disruption. This also includes any fault detection and reduced maintenance costs.
- Space analysis
Reducing operational costs with high-level insights into occupancy patterns can help to optimise the use of space and resources across facilties. By collecting and analysing environmental condition data, businesses can identify potential risks, improve workplace safety, and help prevent accidents before they occur. These capabilities provide the foundation for a smarter, more connected facility, enabling organisations to adapt to evolving industrial trends and drive long-term operational improvements.
The future is connected
Connected LED lighting solutions are transforming industries and factories/warehouses into more efficient, sustainable, and connected/digital spaces. From energy savings and automated controls to adaptive lighting and enhanced safety features, the benefits of connected lighting systems are multifaceted.
As industries continue to embrace digital transformation, connected lighting is emerging as a crucial component in optimising operational processes, reducing costs, and creating safer and more productive work environments.
Learn more about Signify Interact and what it can do for your manufacturing facility: Interact IoT lighting | Interact
Building, Design & Construction Magazine | The Choice of Industry Professionals